🧪 Reflux Partial Condenser Sizer (Dephlegmator)
Size vertical reflux partial condensers and dephlegmators: Hewitt & Wallis flooding limit velocity, Silver-Bell-Ghaly heat transfer, and overhead vapor enrichment.
⚡ Fortran 90 Engine
Double Precision (IEEE 754)
✓ ISO / ASME Validated
 Heat Exchangers
📊 Solver Telemetry
● ACTIVE
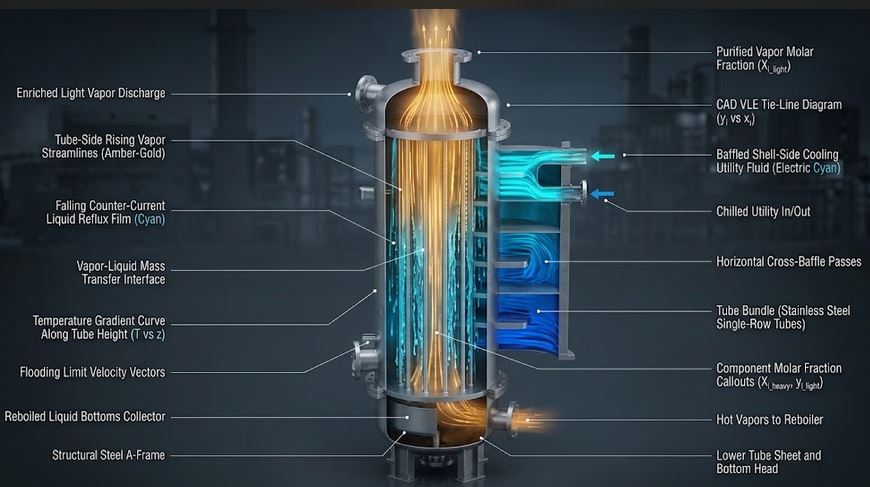
⚡ Counter-Current Vapor Ascent & Falling Liquid Reflux
Real-time visual simulation: Upward rising binary vapor, falling condensate reflux, and overhead purified vapor📝 Configuration & Presets
🌾 Bioethanol Column Top
🧪 Methanol Stripper Reflux
🛢️ Aromatics Benzene-Toluene
💊 Pharma Acetone Recovery
Hewitt & Wallis Flooding Model:
• Flooding Velocity Limit: Vflood = 0.85 · √[g·Di·(ρL−ρv)/ρv] · [1 + (ρv/ρL)1/4·(ṁL/ṁv)1/2]-2
• Flooding Margin: (Vactual / Vflood) · 100% < 80% (Safe operation)
• Silver-Bell-Ghaly Condensation: 1/U = 1/hcond + Z/hgas + tw/kw + 1/hcool.
• Flooding Velocity Limit: Vflood = 0.85 · √[g·Di·(ρL−ρv)/ρv] · [1 + (ρv/ρL)1/4·(ṁL/ṁv)1/2]-2
• Flooding Margin: (Vactual / Vflood) · 100% < 80% (Safe operation)
• Silver-Bell-Ghaly Condensation: 1/U = 1/hcond + Z/hgas + tw/kw + 1/hcool.
📊 Performance Results
📊 Output Summary
Enriched Overhead Vapor Purity
77.8 mol% (Enriched)
Inlet: 70.0% | Duty: 257.7 kW
SAFE COUNTER-CURRENT FLOW
Flooding Limit Approach
35.0%
V = 2.19 m/s / Vfl = 6.25 m/s
Reflux Condensate Return
2275 kg/h
65% reflux split
Overhead Distillate Vapor Flow
1225 kg/h
Purified top product
Overall U-Value (Silver-Bell)
405 W/(m²·K)
140 vertical tubes
📈 Flooding % vs Number of Vertical Tubes Nt
📊 Overhead Purity ytop (mol%) vs Reflux Fraction
=================================================================
 THERMOFLUIDCALC — REFLUX CONDENSER (DEPHLEGMATOR) REPORT
=================================================================
Case Title                 : Aromatics Benzene-Toluene Column Dephlegmator
Binary Mixture             : Benzene-Toluene (Petroleum Aromatics Fractionator)
Vapor Feed Conditions      : mvap = 3500.0 kg/h, Tv = 92.0 C, yin = 70.0 mol%
Condenser Geometry         : Nt = 140 tubes, Di = 38.0 mm, L = 4.00 m
-----------------------------------------------------------------
VAPOR VELOCITY / FLOOD LIM : 2.19 m/s / 6.25 m/s
FLOODING APPROACH MARGIN   : 35.0% (SAFE COUNTER-CURRENT FLOW)
OVERHEAD VAPOR PURITY      : 77.80 mol% (Enriched from 70.0%)
Reflux Condensate Flow     : 2275.0 kg/h
Overhead Distillate Flow   : 1225.0 kg/h
THERMAL CONDENSER DUTY (Q) : 257.74 kW
Overall Heat Transfer (U)  : 405.0 W/(m2.K)
=================================================================
📘 Calculation Methodology & Dephlegmator Standards
Internal Distillation Action
In a reflux partial condenser (dephlegmator), the counter-current contact between upward rising vapor and descending condensate film provides additional theoretical distillation stages, significantly enriching the overhead vapor.
Hewitt & Wallis Flooding Limit
High upward vapor velocities can bridge the tube diameter and prevent liquid reflux from descending, causing column liquid entrainment and pressure surge.
Key Engineering Assumptions
- Silver-Bell-Ghaly multicomponent partial condensation resistance model.
- Rayleigh fractionation equilibrium enrichment.
- Widely used in bioethanol distillation, solvent recovery, and petrochemical fractionators.